
Downstream Oil and Gas: Why Torque Control Moves From Threads to Flanges
Refining and petrochemicals read through their joints: welded spools, bolted flanges and small-bore threads, what torque control means when the joint is a flange, and where the upstream practice of the recorded torque shows up in a refinery.
Downstream oil and gas is the refining, petrochemical and product marketing sector: crude and gas liquids become fuels, feedstocks and chemicals. Its plants are built from welded process piping joined at bolted flanges, so torque control there means bolt torque under ASME PCC-1, not make-up torque on threads. There is no threaded tubular to buck, and no bucking unit in the sector.
At a glance
| What downstream does | Refines crude oil into fuels and intermediates, converts gas liquids and naphtha into petrochemicals, stores, blends and distributes the products |
| The piping | Process piping designed and built under ASME B31.3, fabricated into welded spools, erected and joined at bolted flanges; small-bore threaded piping in limited services |
| The joints | Butt welds, which are permanent; bolted flanges, which are opened for maintenance; threaded small-bore joints made up with a wrench. None is a tubular make-up in the upstream sense |
| Where torque control lives | On the flange: lubricated studs, a tightening pattern, staged passes to a target, calibrated tools and a joint record, following ASME PCC-1 and the plant’s own bolting programme |
| Decision this page supports | Recognising a downstream torque requirement for what it is, bolting rather than bucking, and directing it to the right equipment and the right people |
What downstream is
A refinery takes crude oil that arrived by pipeline or tanker and separates it, converts it and treats it until it leaves as gasoline, diesel, jet fuel, fuel oil, lubricant base stock, asphalt and a set of intermediates. A petrochemical complex takes naphtha, ethane or other feedstocks and cracks them into ethylene, propylene and the building blocks of plastics, fibres and fertilisers. Terminals, blending plants and distribution networks carry the products to customers. The sector guides describe it as the final step of the chain, where crude oil and gas liquids are refined and converted into products for domestic, industrial and transport use (Profire, Upstream, Midstream and Downstream).
The plant itself is a set of process units connected by piping and controlled from a central room. A supplier survey of the sector names the crude distillation unit, fluid catalytic cracker, hydrocracker, catalytic reformer, alkylation unit, sulphur recovery, steam crackers, storage tanks to API 650, loading racks and flare systems among its equipment (Projectmaterials, Oil and Gas Equipment by Sector). What that list does not contain is a single threaded tubular in the upstream sense. There is no casing, no tubing, no drill string and no downhole tool anywhere in a refinery, and the reason is worth understanding before a supplier of make-up equipment answers a downstream enquiry.
Three joints, none of them a tubular make-up
Process piping in a refinery is designed to ASME B31.3, the process piping code, and it is joined in three ways. Spools are fabricated by butt welding pipe, fittings and flanges together in a shop; those spools are erected and connected to each other and to equipment nozzles at bolted flange joints; and small-bore branches, instrument connections and utility lines may be threaded, made up on a taper thread with sealant to an engagement rule. Each joint is a different trade with a different owner.
| Joint | How it is made and controlled | What that means for a make-up equipment supplier |
|---|---|---|
| Butt weld | Welded to a qualified procedure by a qualified welder, inspected by radiography or ultrasonics, permanent by design | Nothing to offer. Welding equipment and inspection are a different supply base |
| Bolted flange | Gasket between two flanges, compressed by a ring of studs tightened in a pattern to a target load; opened and re-made every turnaround | The torque work of the sector, but it is bolt torque with wrenches, hydraulic torque tools or tensioners, under a bolting programme |
| Threaded small-bore | Tapered pipe thread with sealant, made up with a pipe wrench to an engagement rule, used where the code allows and the service is benign | No recorded torque, no machine, and no place for one; a wrench and a competent fitter |
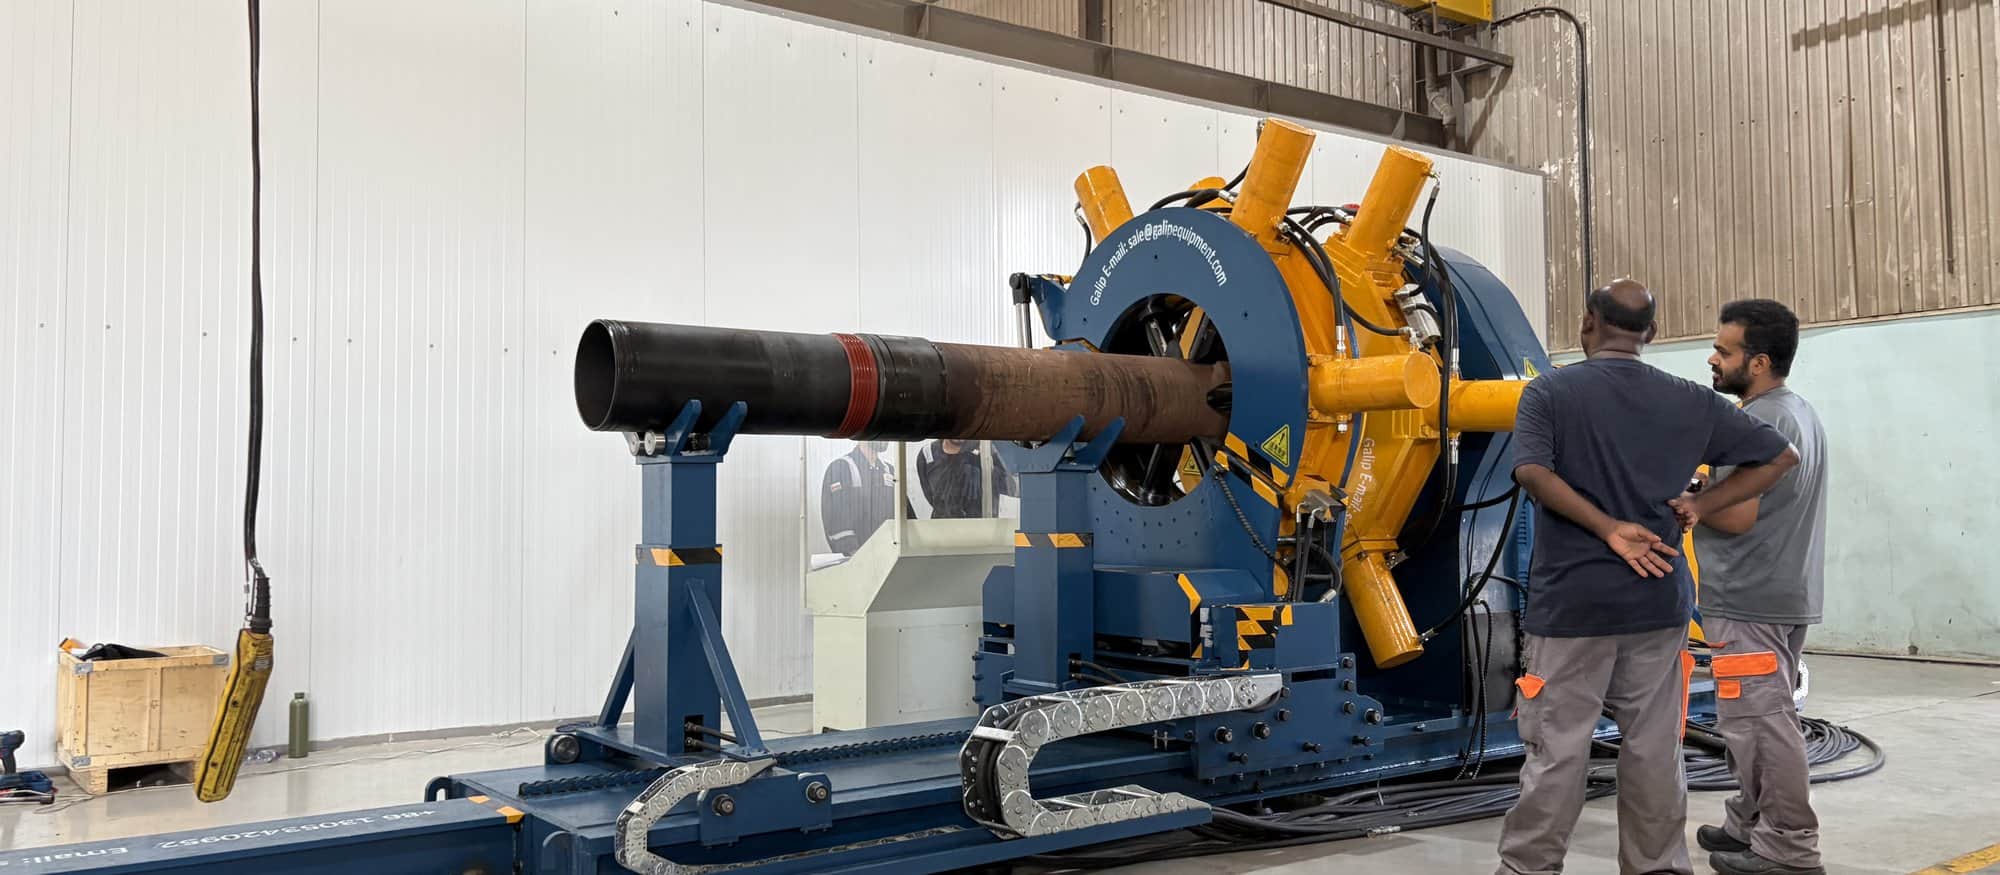
Put the upstream joint beside those three and the difference is obvious. A casing coupling or a tool joint is made up by rotating one threaded member into another under a controlled torque while recording torque against turns, on a connection that will be broken out and remade many times over its life. The joint is the pipe. In a refinery the pipe is welded and the joint is a gasket between flanges; rotation plays no part in it. The machine that makes up the first kind of joint, the hydraulic bucking unit, has no work in a plant built from the second and third kinds.
Bolted flange joint assembly: torque control downstream
None of that means downstream is casual about torque. A leaking flange on a hydrocarbon unit is a fire hazard, and the industry has treated flange assembly as a controlled process for a long time. ASME PCC-1, Guidelines for Pressure Boundary Bolted Flange Joint Assembly, is the reference document. It covers the training and qualification of bolting personnel, joint preparation and inspection, gasket handling, lubrication, the tightening pattern and the number of passes, target torque or bolt stress, the tools and their calibration, and the records; and it ties its service categories to the fluid service categories defined in ASME B31.3 (ASME PCC-1).
The aim of all that is not torque for its own sake. Torque is a means of stretching the studs so that the gasket is compressed evenly around the flange and stays compressed through pressure and temperature cycles. Because friction between the nut and the stud eats a large and variable share of the applied torque, the better programmes control bolt load directly, with hydraulic tensioners or by measuring stud elongation, and use torque as the practical surrogate where that is not feasible. Either way the tool is calibrated, the sequence is written down, the passes are staged, and the finished joint carries a tag or a record that says who assembled it, with what, to what.
A refinery mechanical department therefore has a torque procedure every bit as formal as a threading shop’s, and a maintenance planner who asks a bucking unit supplier about torque tools is usually asking about that programme. The right answer is a referral to bolting equipment suppliers, and an explanation of why: the two disciplines share a word and a habit, and nothing else.
The habit that crosses the sector line
That habit is traceability. A flange joint record in a refinery names the joint, the gasket, the stud material, the lubricant, the target, the tool, the calibration certificate and the assembler. A torque-turn record in an upstream threading shop names the joint, the connection, the compound, the target, the machine, the sensor calibration and the operator. Both exist for the same reason: when a joint fails, somebody will ask what was done and by whom, and a number in a book beats a memory.
The weak point in both records is the same as well. A recorded torque is only as good as the sensor that measured it, and the sensor is only as good as its last calibration against a reference that can itself be traced. How an upstream workshop keeps that chain unbroken, for its torque sensors and its load cells, is set out in torque and load calibration; a refinery bolting programme applies the same logic to its torque wrenches and tensioners, and a turnaround audit will ask for the certificates in exactly the same way. If there is one thing an upstream equipment supplier can honestly claim to share with a downstream customer, it is that chain.
Where downstream and upstream actually touch
The sectors meet in three places, and none of them brings a bucking unit into a refinery. The first is the wellhead and production facility, upstream’s own downstream edge, where threaded tubing hangers sit a metre from flanged trees and separators; the completion crew makes up the tubing and the wellhead technician bolts the flanges, each to their own document. The second is the gas plant, formally midstream, whose piping and bolting look exactly like a refinery’s. The third is the workshop that supplies both: a large engineering contractor may fabricate refinery spools in one bay and service downhole tools in another, and its quality system holds a bolting procedure and a make-up procedure side by side without confusing them.
The value chain overview on this site, upstream, midstream and downstream oil and gas, draws the same line from the other direction, and the midstream page explains the one place a thread survives beyond the well, on small gathering lines. Downstream has no such exception. A supplier who claims a threaded tubular make-up machine belongs in a refinery has misread the sector, and a buyer who receives such a claim should treat it as a sign the supplier does not know the industry.
When another page is the better start
A refinery or petrochemical maintenance reader has, by this point, learned that the equipment they need is bolting equipment and should be talking to that supply base and to ASME PCC-1. An engineering contractor with both a spool shop and a tool workshop should read the downhole tool service centre guide for the make/break side and keep its bolting procedure where it is. A buyer whose question was really about which upstream workshops use a make-up machine should be on the upstream page of this series, which walks through the phases of a well and who owns each connection.
There is one more reader worth naming: the upstream workshop that has been asked by a downstream customer to test or make up something threaded, a large valve stem, a pump coupling, a heat exchanger part. Occasionally such work fits a bucking unit and the large threaded assemblies guide describes when it does. The test is whether the job is a controlled rotation of one threaded member into another to a recorded torque. If it is, the machine may apply. If it is a flange, it never does.
Frequently asked questions
What is downstream oil and gas?
Downstream is the sector that turns crude oil and gas liquids into products: refineries, petrochemical plants, blending and storage terminals and the distribution of fuels and chemicals. It sits at the end of the value chain after upstream production and midstream transport, and its plants are built from welded process piping joined at bolted flanges.
Does a refinery use bucking units?
No. A bucking unit makes up and breaks out threaded tubulars, and a refinery contains none: its piping is welded into spools and bolted together at flanges under ASME B31.3. The torque discipline in a refinery is bolted flange joint assembly under ASME PCC-1, done with torque wrenches, hydraulic torque tools and tensioners by bolting crews.
What is ASME PCC-1?
Guidelines for Pressure Boundary Bolted Flange Joint Assembly, published by ASME. It covers the qualification of bolting personnel, joint and gasket preparation, lubrication, tightening patterns and passes, target torque or bolt load, tool calibration and joint records, and it relates its service categories to the fluid service definitions in the ASME B31.3 process piping code.
Why is bolt torque different from make-up torque?
Make-up torque rotates one threaded tubular member into another to seat a shoulder or seal, and the torque-turn curve is the evidence. Bolt torque stretches a ring of studs to compress a gasket between two flanges, and torque is only a surrogate for bolt load because friction takes a large, variable share. Different joint, different physics, different tool.
Is there any threaded piping in a refinery?
Yes, in small-bore lines, instrument connections and utility services where the piping code allows it. Those joints are tapered pipe threads made up with sealant and a wrench to an engagement rule. They carry no recorded torque and no machine is used for them, so they are unrelated to the controlled make-up of casing, tubing or tool joints.
Where do upstream and downstream torque work overlap?
In the habit of traceability. Both sectors record who assembled a joint, with which tool, to which target, and both depend on that tool having a calibration certificate traceable to a reference. The joints differ entirely, flange studs against threaded tubulars, but a calibration audit asks the same questions of a refinery bolting crew and a threading shop.
Send the joint description with the enquiry
A torque enquiry from a downstream plant can be answered in one exchange if it describes the joint. State whether the joint is a bolted flange, in which case the answer is a bolting programme and bolting equipment, or a threaded assembly that rotates together, in which case the useful details are the outside diameter and length of the parts, the thread type, the expected make-up and break-out torque, whether a torque record is required, the site power supply and the bay available. The Galip team will say plainly which of the two it is.
The downstream checklist
- Identify the sector: refining, petrochemicals and product distribution are downstream; a gas plant is midstream; a wellhead is upstream, however flanged it looks.
- Identify the joint: butt weld, bolted flange or threaded small-bore. None of them is a tubular make-up.
- If the question is torque on a flange, the reference is ASME PCC-1 and the plant’s bolting programme, and the equipment is bolting equipment.
- If the question is a threaded assembly that rotates together to a recorded torque, describe it fully and it can be assessed against a bucking unit.
- Whatever the joint, check that the tool that measured the torque or load has a traceable calibration certificate; that requirement is the same in every sector.
- Keep the two procedures, bolting and make-up, in separate documents even where one workshop does both.
- Treat any claim that a threaded tubular make-up machine belongs in a refinery as a sign to check the supplier’s understanding of the industry.
Expert Consultation
Need more information on optimizing your equipment performance? Our engineering team is available for technical consultations.
Request a Quote
Tell us about your requirements and our engineering team will prepare a detailed proposal with specifications, pricing, and delivery timeline.
